In the process of steel production, a large number of blast furnace gas, converter gas, coke oven gas, rich in carbon monoxide, hydrogen and methane are valuable components, which are the main secondary energy sources of steel works. 55-60% of H2 is contained in coke oven gas, converter gas and blast furnace gas respectively containing 60% ~ 60% and ~25% CO, so steel exhaust completely can be used as a source of chemical synthesis of CO and H2 needed.
BFG to CO
Separation of CO from blast furnace gas is an international problem, which is mainly due to the blast furnace gas also contains a large number of N2 and CO2. Because of the close boiling point of N2 and CO, the traditional cryogenic rectification process can not be used to separate CO from blast furnace gas. The adsorption of CO and N2 is low, and the adsorption of CO2 is easy to poisoning and deactivation, so the conventional pressure swing adsorption method can not be used for CO separation of blast furnace gas.
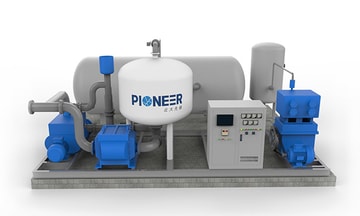
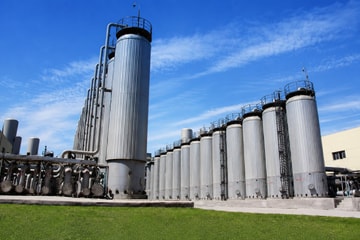
PIONEER, on the basis of its mature and leading PSA technology, according to the characteristics of blast furnace gas, developed the process of the formation of a unique CO separation technology of blast furnace gas, by which blast furnace gas can be used from the low cost of mass separation CO. The enriched CO gas can be used for the following three purposes:
1. To produce high value-added chemical products
CO is a kind of important raw material with chemical synthesis which can be purified to 99% from the blast furnace for the production of ethylene glycol, acetic acid, dimethyl carbonate, polycarbonate, TDI, DMF and other chemical products, thus significantly enhancing the added value of the gas. To obtain CO by the use of blast furnace gas has a large cost advantage. With the rapid development in the non-steel industry, it has attracted attention by many domestic and overseas famous iron and steel enterprises.
2. To be premium fuel
The carbon monoxide purified up to 70% from blast furnace, whose heat value is up to 8200kj/nm3, can replace the coal and natural gas for metallurgy, such as the combustion section in iron making links.
3. To be reducing gas of blast furnace injection
The research shows that, to increase concentration of CO from the blast furnace gas and converter gas to above 45%, by the use of separation technology, and then to inject into the blast furnace will significantly improve the carbon monoxide and hydrogen content of the furnace, and indirect reduction acceleration of the sinter in the furnace shell, which helps improve the production and heat efficiency.
Economic Benefit Analysis
PIONEER makes the following calculation according to the present coal-chemistry industry situation. To produce 1m3 CO with high purity by separation and purifying of CO from coal gas cost ¥2.00 at current price of coal, but it only cost less than ¥1.00 to produce 1m3 CO with high purity by separation and purifying of CO from BFG with PKU PIONEER’s technology . This means PKU Pioneer can save 50% of the CO producing cost than coal gas making.
Successful Cases
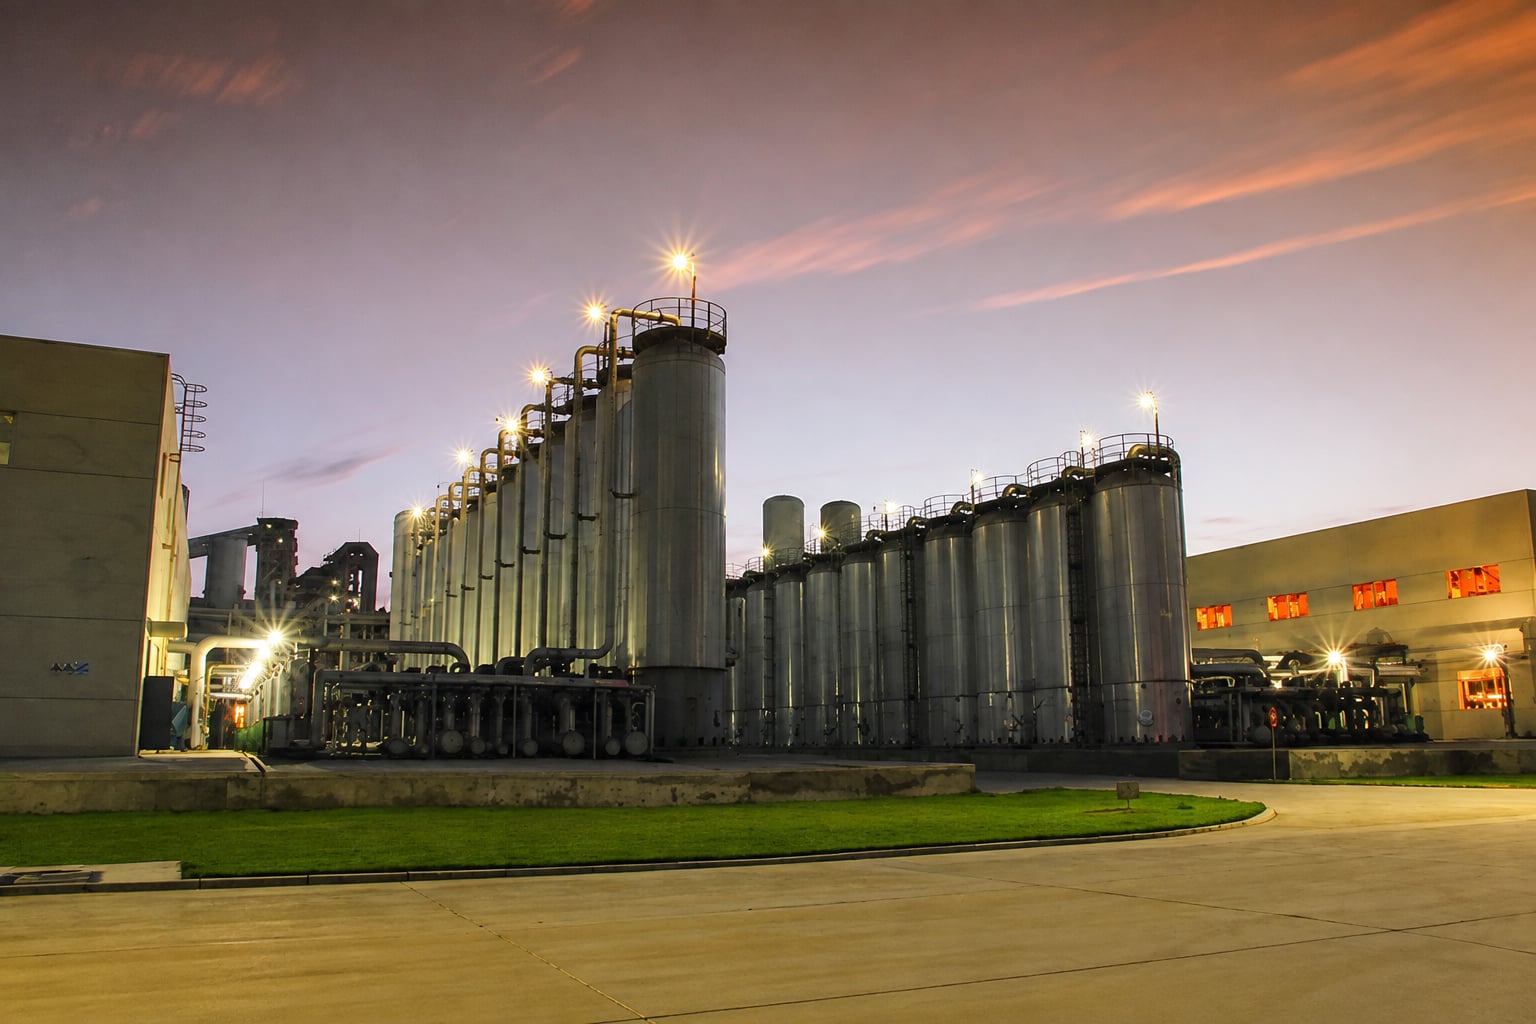
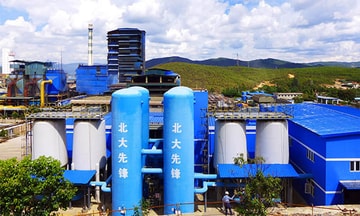
This technology has been implemented in Hengyang Steel Group. The project extracted product CO (17,500Nm3/h, 70%) from BFG of 67,000Nm3/h. CO enriched will be used as an alternate to natural gas and weighs 30% of total gas consumption at full capacity. It created significant economic benefits to the enterprise, and the elimination of the BFG emission, and a significant reduction in carbon emissions.
Converter Gas to CO
Separation of CO from converter gas is an international problem, which is mainly due to the converter gas also contains a large number of N2 and CO2. Because of the close boiling point of N2 and CO, the traditional cryogenic rectification process can not be used to separate CO from converter gas. The adsorption of CO and N2 is low, so the conventional pressure swing adsorption method can not be used for CO separation of converter gas.
Based on mature and leading PSA CO technology and the characteristics of converter gas, PKU PIONEER has developed the process of the formation of a unique CO separation technology of converter gas, which can be applied to get over 99% purity of CO product in large capacity from converter gas economically. The enriched CO gas can be used for producing high value-added chemical products.
CO is a kind of important raw material with chemical synthesis. It can purify CO from the converter gas to over 99%, which is used for the production of ethylene glycol, acetic acid, dimethyl carbonate, polycarbonate, TDI, DMF and other chemical products, thus significantly enhancing the added value of the gas. To obtain CO by the use of converter gas has a large cost advantage. With the rapid development in the non-steel industry, it has attracted attention by many domestic and overseas famous iron and steel enterprises.
Economic Benefit Analysis
The remained converter gas can be used for electricity generation except for converter fuel gas use. However, because its calorific value is low, the value added for electricity generation is low, and at the same time the carbon emission is high. The purified CO for chemical synthesis not only can decrease the investment of that from fossil raw material, but also can increase the added value and decrease the carbon emission. It is friendly environmental.
Successful Case
This technology has been applied to Shandong Aside Technology Company, and the flow of the converter gas is 45000 Nm3/h for 18000 Nm3/h CO product, of which the purity is 98.5%. This application is for 200000 t/a methane acid and 50000 t/a oxalic acid. Compared with the converter gas for electricity generation use, 318 thousand tons carbon emission can be saved per year.